The 8 methods of non-destructive testing: a comprehensive overview
Non-destructive testing (NDT) covers methods for testing materials and components for defects without damaging them. This article presents the eight most important NDT methods – including visual testing (VT), ultrasonic testing (UT), radiographic testing (RT) and magnetic particle testing (MT) – with their advantages, limitations and typical applications. Inspection drones such as the Flyability ELIOS 3 mainly support visual testing: they take the camera to hard-to-reach places without personnel having to go there.
NDT: inspect components without damaging them
Non-destructive testing (NDT) covers a wide range of test methods that make it possible to test the condition of materials and components for defects and weak points without impairing their structure or functionality. These test methods are of central importance because they allow safety-relevant information to be gathered without destroying or altering the object under test. Particularly in safety-critical industries such as aerospace, construction, oil and gas and power generation, NDT is indispensable for ensuring the integrity and longevity of components and systems.
NDT allows components to be monitored regularly throughout their entire life cycle. Early detection of material fatigue, cracks or corrosion allows companies to carry out preventive maintenance and thus avoid serious failures or accidents. NDT also reduces downtime and saves costs by minimising expensive spare parts and complex repairs.
The range of NDT methods extends from simple visual inspections to sophisticated techniques such as ultrasonic and radiographic testing, which can detect deeper-lying defects. The eight most important NDT methods are presented in detail below, including their specific advantages and areas of application in industry today.
 Christian Engelke
1. Visual testing (VT)
Visual testing (VT) is the most fundamental and most widely used NDT method. It makes it possible to detect visible defects on the surface of a component simply by looking or with the aid of optical tools. These include cracks, deformation, corrosion or other surface anomalies. Visual inspection can be carried out directly with the eye or indirectly using mirrors, endoscopes or video equipment.
Application:
Visual testing is often carried out as the first step in inspections and complements other testing methods that focus on deeper defects. In practice, visual inspection can be used in many areas: from the inspection of welds and concrete and steel structures to pipelines and pressure vessels. It is also widely used in aviation to check critical components such as wings and fuselages for visible defects.
Use of technology:
With the development of drone and robot technology, visual testing has changed considerably. One example is the internal inspection drone Flyability ELIOS 3, which makes it possible to carry out visual inspections in hazardous or hard-to-reach areas. This drone can fly into confined spaces such as tanks or pipes and capture images, videos and 3D data there without inspectors having to enter these hazardous places. Scaffolding and man entry are not needed.
Advantages:
- Simple and cost-effective
- No special equipment required
- Immediate results
- Can be combined with advanced technologies such as drones
Limitations:
- Only suitable for visible defects
- Dependent on lighting conditions and the experience of the inspector
- Cannot detect internal or deep-lying defects
2. Ultrasonic testing (UT)
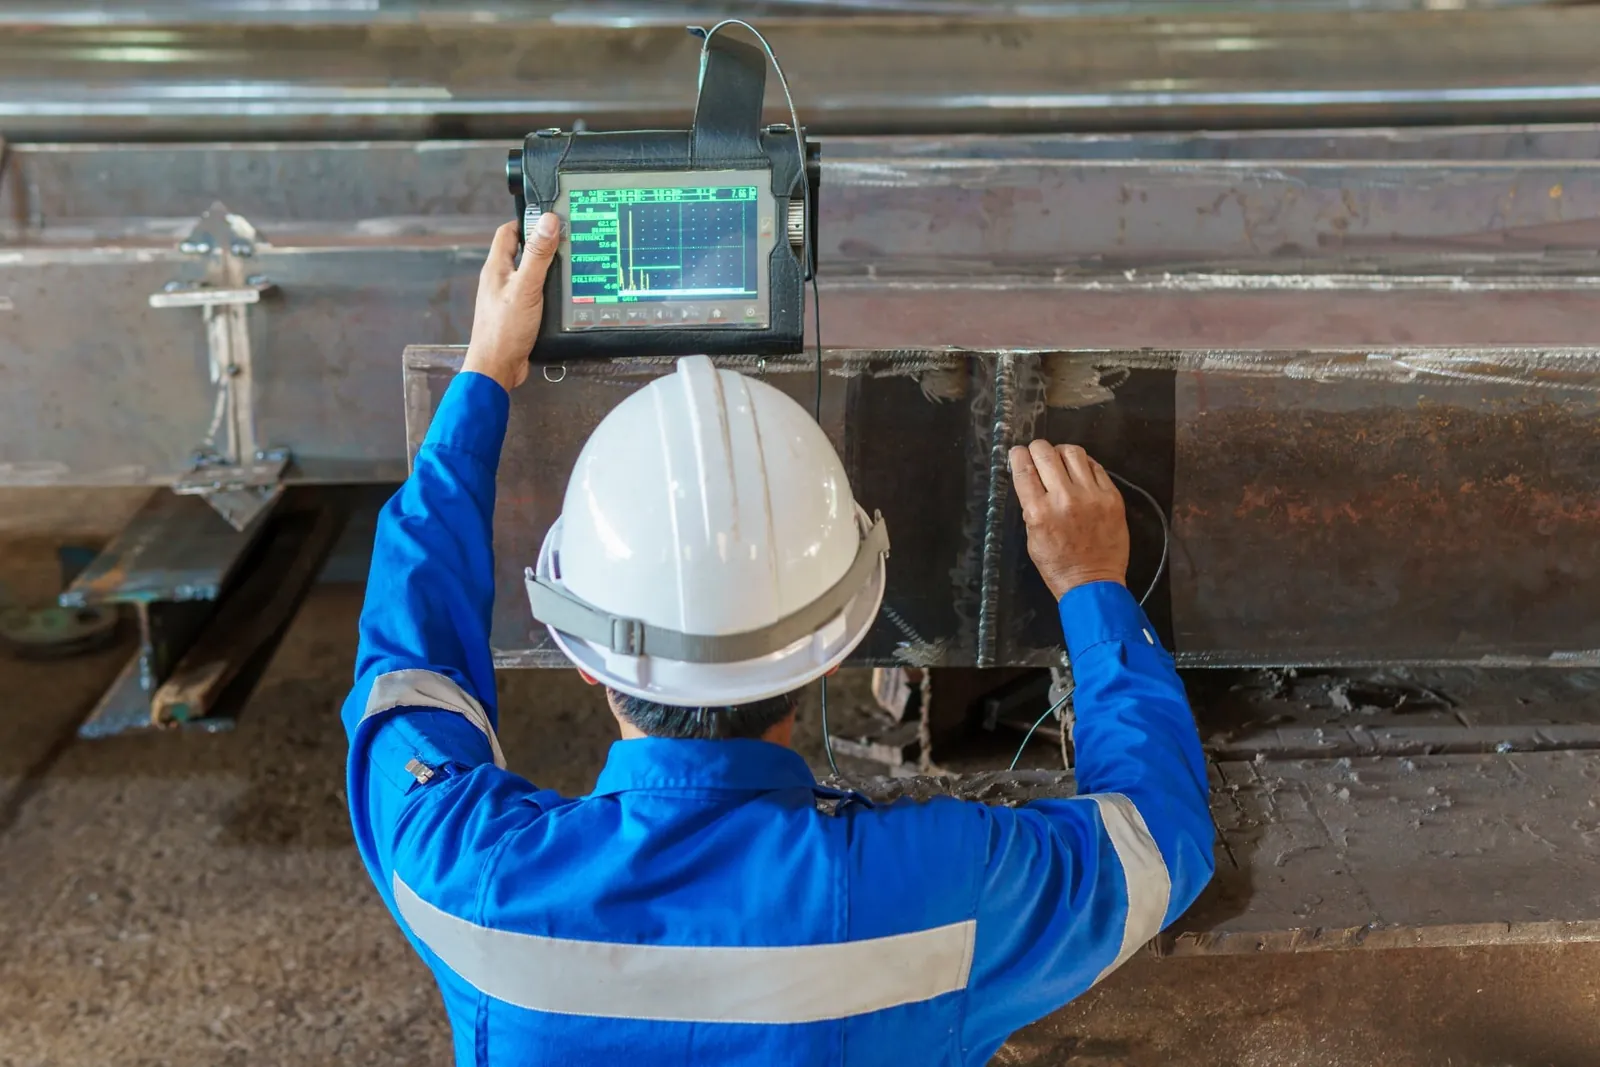
Ultrasonic testing (UT) is one of the most important NDT methods and makes it possible to identify defects inside a material. High-frequency sound waves are sent through the material. The waves are reflected at interfaces, such as cracks or other irregularities, and the reflected signals are picked up by a receiver. This method is particularly effective for thick-walled materials and is often used to inspect welds, pipes and pressure vessels.
Application:
Ultrasonic testing is used in a wide range of industries. In the aviation industry, for example, it is used to identify cracks in aircraft wings or fuselages that can result from material fatigue. In the oil and gas industry, UT is used to detect corrosion in pipelines or defects in welds.
Technique:
UT uses a probe that generates and receives sound waves. This probe is often used in direct contact with the material, with a couplant (usually a gel) applied to optimise the transmission of the sound waves. There are also more advanced variants of UT, such as phased array ultrasonic testing (PAUT), which allows a more detailed and accurate representation of defects.
Advantages:
- High precision and depth resolution
- Can be used on thick materials
- Suitable for detecting deep-lying defects
- Can be automated for high-volume inspections
Limitations:
- Requires special equipment and well-trained inspectors
- Limited with coarse-grained materials such as cast iron
- Coupling to the surface and calibration required
3. Radiographic testing with X-rays and gamma rays (RT)
Radiographic testing (RT) uses electromagnetic radiation (X-rays or gamma rays) to see through the internal structure of a material. As with a medical X-ray, the radiation is sent through the material and an image or "shadow" is produced on a detector. This makes internal defects such as pores, inclusions or cracks visible that cannot be seen from the outside.
Application:
RT is often used to inspect welds in critical applications such as pressure vessels and pipelines. In aerospace, this method is used to check the integrity of metal components, while in the automotive industry castings are tested for internal defects.
Technique:
The components to be tested are placed between a radiation source and a detector. X-rays penetrate the material and produce an image of the internal structure. Defects such as voids or cracks appear on the image as darker or lighter areas because they absorb the radiation differently.
Advantages:
- Allows detailed testing of the internal structure
- The radiograph also serves as documentation
- Can detect surface and volumetric defects
Limitations:
- Requires strict safety precautions because of radiation exposure
- Relatively expensive and complex to carry out
- Access from both sides of the component is required; wall thickness limits its use
4. Eddy current testing (ET)
Eddy current testing (ET) is an electromagnetic method used to detect surface and near-surface defects in electrically conductive materials. A changing magnetic field is generated in the component, inducing eddy currents. Defects that disturb the flow of these currents are detected.
Application:
Eddy current testing is particularly well suited to inspecting non-ferrous metals such as aluminium or copper, which are widely used in the aerospace industry. Typical applications include the inspection of fuselages, welds and engines.
Technique:
A coil is passed over the component to generate a magnetic field. The induced eddy currents flow through the material, and any defects cause changes in the magnetic field that are picked up by the test coil. The coil does not have to touch the component, and the test involves little effort.
Advantages:
- No couplant needed; the probe is passed directly over the surface at a small distance.
- Suitable for conductive materials
- Can detect surface and near-surface defects
Limitations:
- Limited penetration depth, only for surface and near-surface defects
- Not suitable for non-conductive materials
- Requires special calibration and highly sensitive equipment
5. Magnetic particle testing (MT)
Magnetic particle testing (MT) is used to detect surface and near-surface defects in ferromagnetic materials. This method is based on inducing a magnetic field in the material. Defects disturb the flow of the magnetic field, and iron particles applied to the surface collect at the defects and make them visible.
Application:
Magnetic particle testing is often used in the automotive industry to inspect castings and in heavy industry to check welds. The method is also widely used in the inspection of pressure vessels and pipelines.
Technique:
The material is magnetised, and iron particles or a magnetic powder are then sprinkled onto the surface. The particles collect at defects such as cracks or notches and make them visible to the inspector.
Advantages:
- Simple to carry out
- Cost-effective
- High sensitivity to surface defects
Limitations:
- Only suitable for ferromagnetic materials
- Limited penetration depth
- Visual inspection required to identify defects
6. Penetrant testing (PT)
Penetrant testing (PT) is a method used to detect surface defects. A liquid penetrant is applied to the material and seeps into cracks or pores. After a cleaning stage, a developer is applied, which draws the penetrant out of the defects and makes them visible.
Application:
PT is often used to inspect non-porous materials such as metals, glass and ceramics. Typical applications include testing welds, castings and ceramics in aerospace, the automotive industry and construction.
Technique:
First, the component is thoroughly cleaned to remove all surface contamination. The penetrant is then applied and seeps into surface defects. After the excess penetrant has been removed, a developer is applied that makes the defect visible.
Advantages:
- Inexpensive and easy to use
- High sensitivity to small surface defects
- Wide range of applications on different materials
Limitations:
- Only suitable for surface-breaking defects
- Not suitable for porous materials
- Thorough cleaning required
7. Acoustic emission testing (AE)
Acoustic emission testing uses acoustic signals caused by stress or material fatigue inside a component to detect defects. When a defect grows or a material fails, acoustic emissions occur, which are picked up by special sensors.
Application:
This method is often used to monitor large structures such as bridges, pressure vessels and high-rise buildings in order to detect stress cracks or signs of fatigue at an early stage.
Technique:
Sensors are attached to the surface of the component to detect the sound waves generated by stresses or defects. The strength, frequency and position of the emissions provide information about the condition of the material.
Advantages:
- Can monitor defects in large structures
- Real-time monitoring possible
- Detects dynamic changes in the material
Limitations:
- Requires special sensors and equipment
- Only suitable for active defects (where changes in the material are occurring)
- Low spatial resolution
8. Thermography (TT)
Thermography is a method that uses infrared radiation to measure temperature differences on the surface of a material. These temperature differences can be caused by defects such as cracks or delamination that affect the heat flow in the material.
Application:
Thermography is often used in building inspection to identify leaks, voids or defective insulation. In industry it is used to inspect switchgear, motors and pipelines in order to detect overheating and defects early.
Technique:
An infrared camera is used to record the heat radiated by the material. Areas with conspicuous heat radiation are analysed to determine whether a defect is present.
Advantages:
- Contactless
- Suitable for inspecting large areas
- Detects thermal anomalies that indicate defects
Limitations:
- Detects only defects that show up as a temperature difference on the surface
- Sensitive to ambient conditions
- Limited penetration depth
The drone's visual inspection shows where further NDT methods should be applied
Non-destructive testing (NDT) is an important tool for assessing the condition of materials and components without damaging them. With methods such as visual, ultrasonic or thermographic testing, defects can be detected early and maintenance planned before serious failures occur.
Drones contribute above all to visual testing. The Flyability ELIOS 3 flies into vessels, boilers and confined spaces and captures close-up images and videos there. Its thermal camera also allows thermographic images in cramped areas, and the LiDAR produces a 3D point cloud in which anomalies can be located and deformation identified. Learn more on our page on inspection with the ELIOS 3.
For external areas we use the DJI M30T. With its zoom camera it is suitable for the visual inspection of concrete and steel structures, for example on façades, cooling towers or pipe racks. The radiometric thermal camera shows temperature differences on surfaces and thus possible defects or insulation problems.
The drone inspection is therefore the starting point: it covers visual inspection and damage mapping – in high resolution, at close range and located in the 3D point cloud, without scaffolding or aerial work platforms. Methods applied to the component itself, such as ultrasonic, magnetic particle, penetrant or radiographic testing, are used by the inspector only where they are needed: at the points marked in the inspection report.